Our Factory Facilities
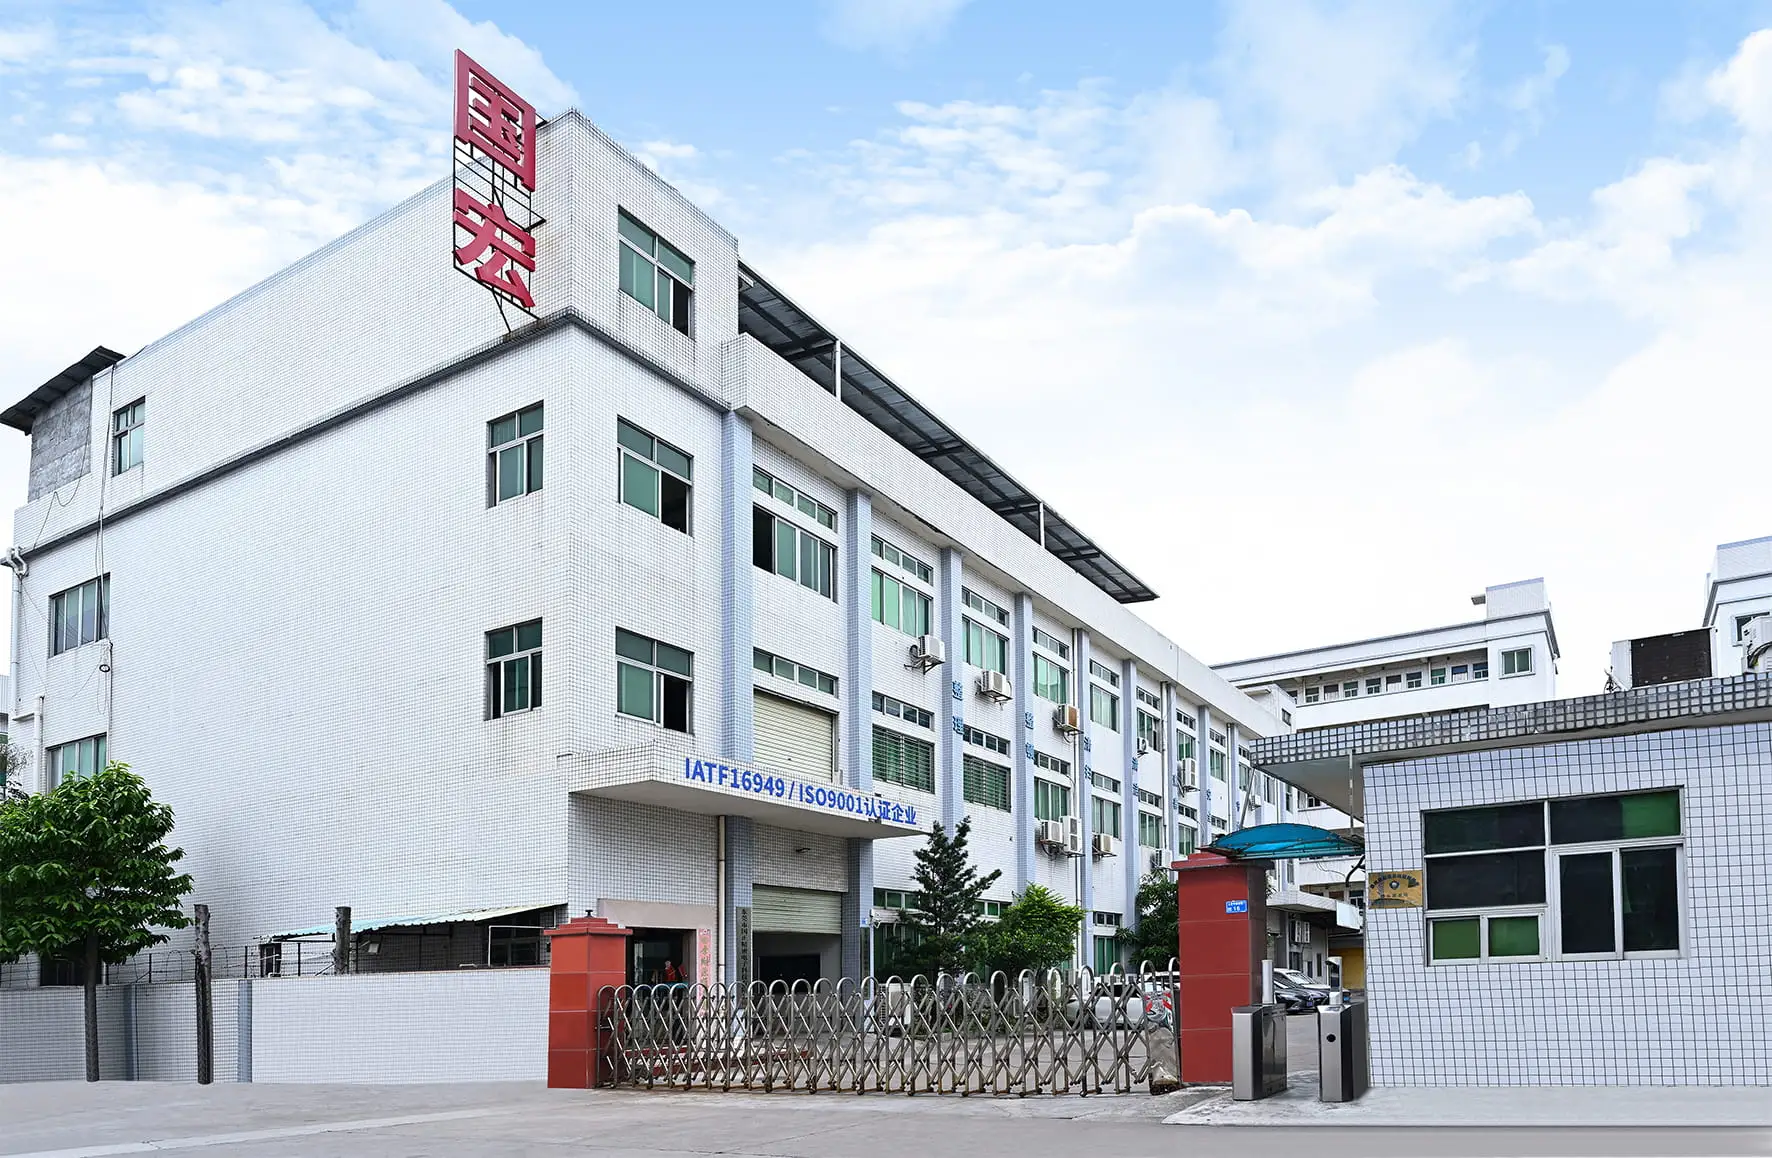
A 10,000 m² factory floor in Dongguan with tooling, molding, stamping, CNC and inspection under one quality system — 280 people, injection molding from 30 to 260 T and 21 high-speed stamping presses running every day.
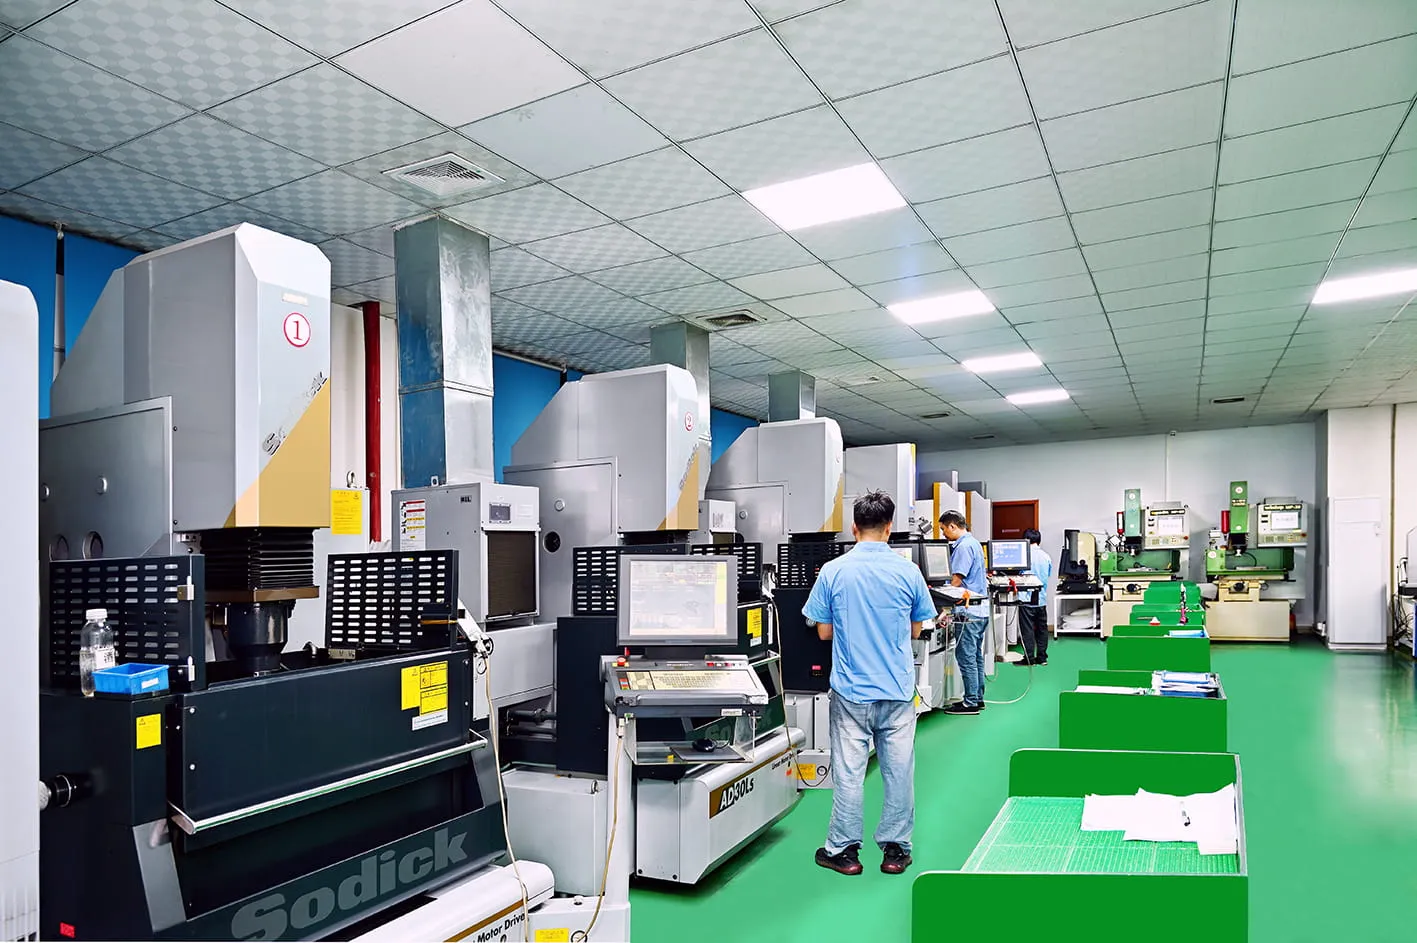
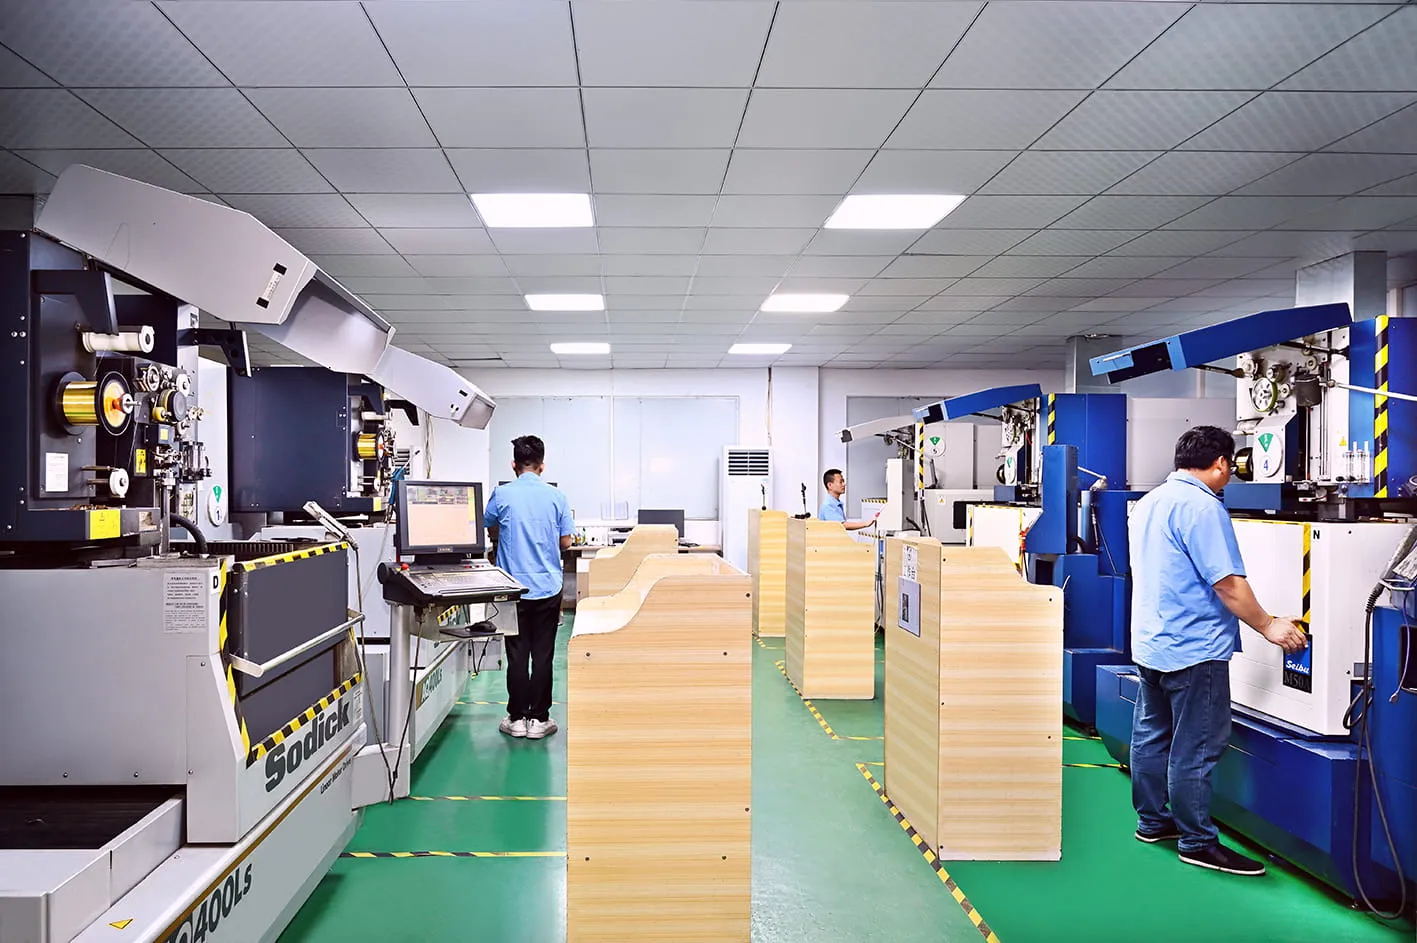
Tooling & EDM
Mold design and steel cutting coordinated through an audited tooling partner network — our own wire EDM, die-sinking EDM and CNC lines handle electrodes, punch and die steel.
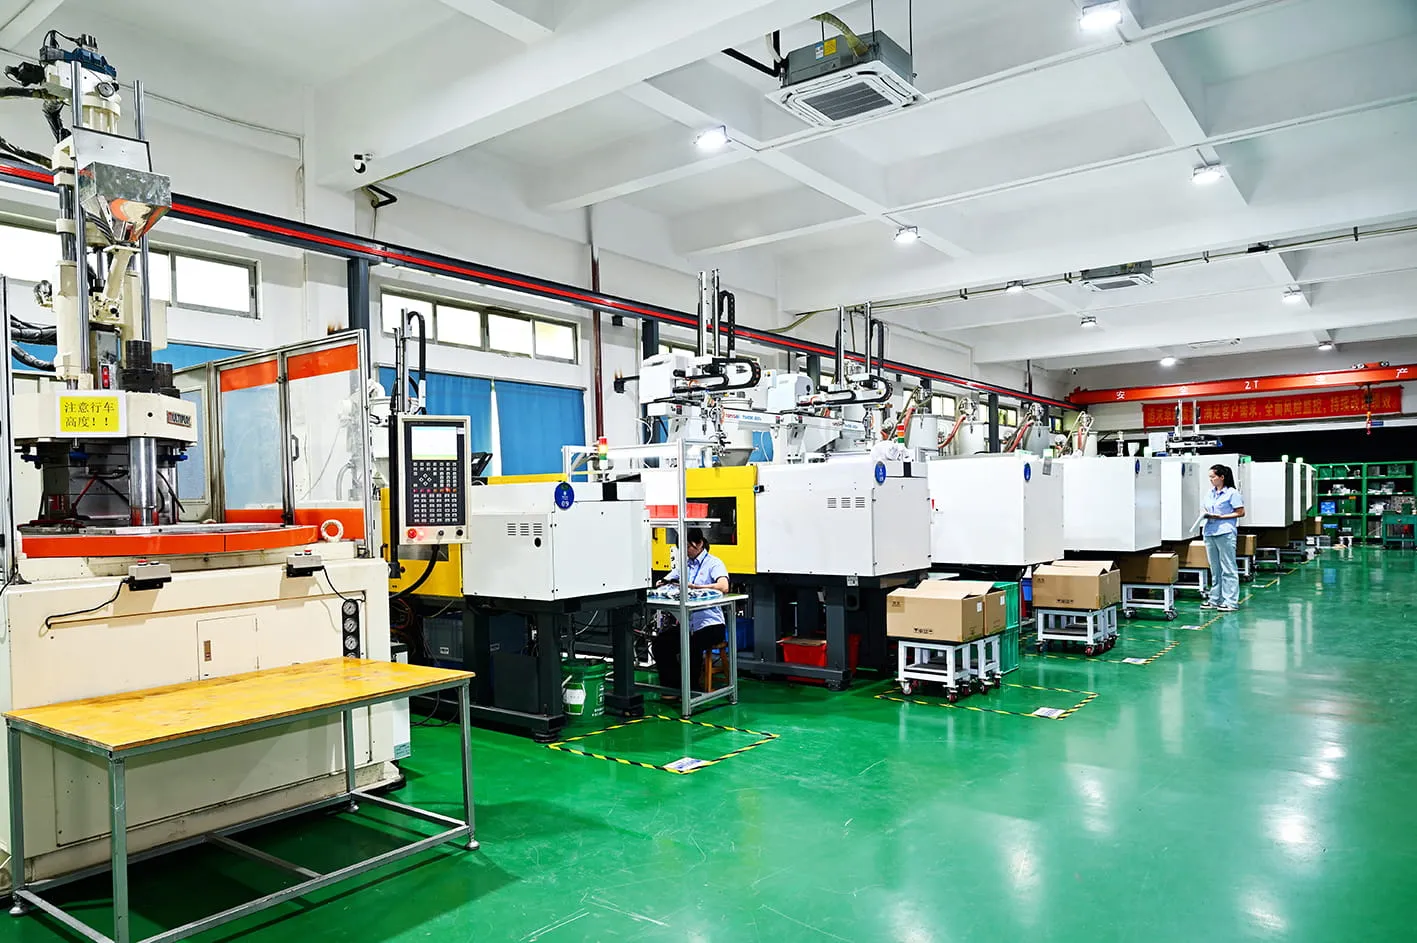
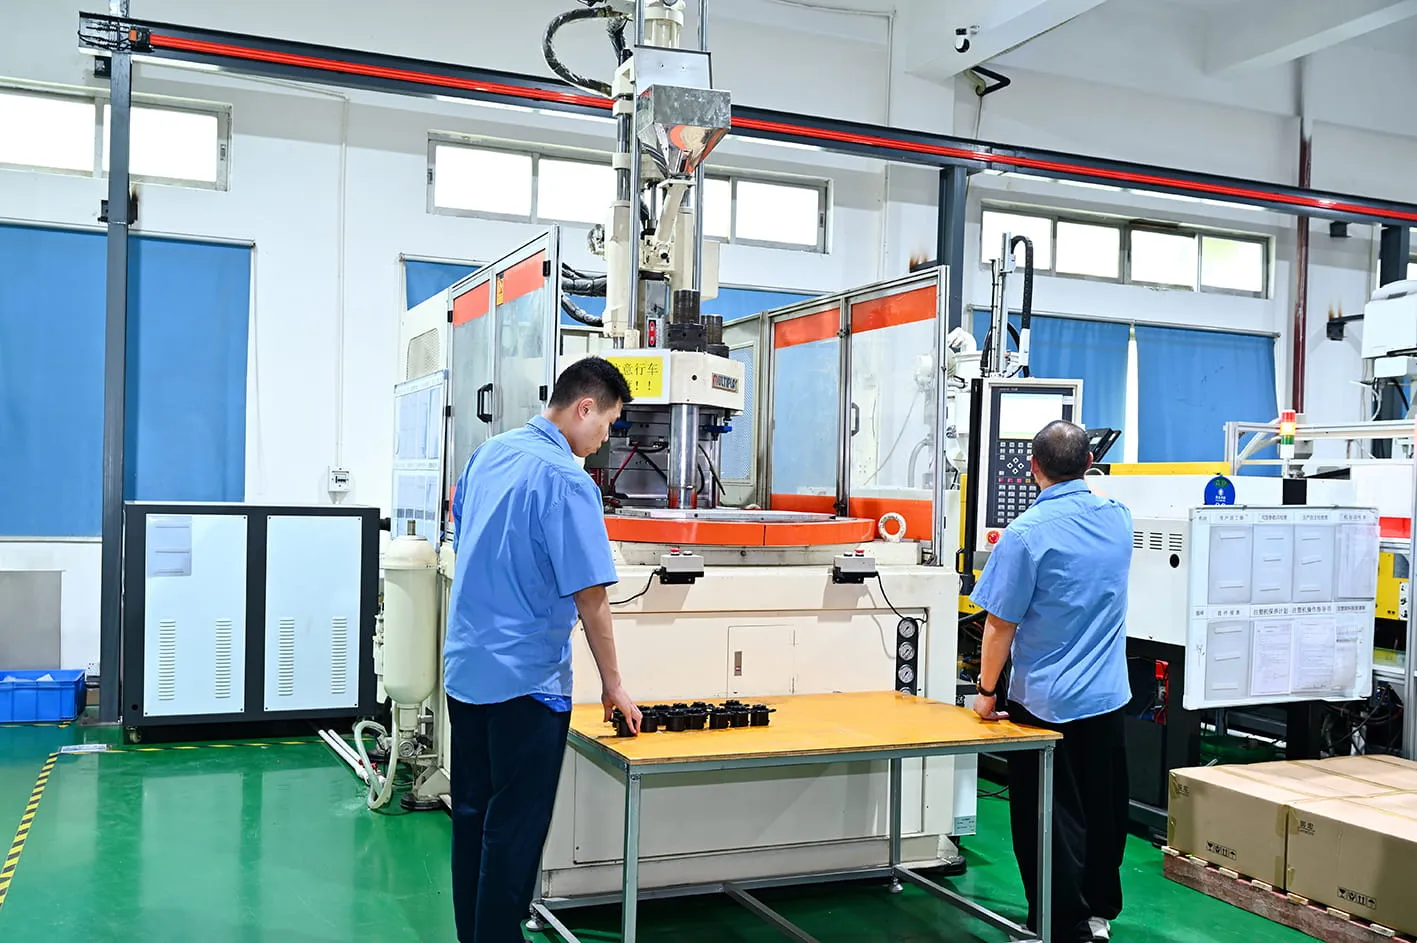
Injection Molding Workshop
Injection presses spanning 30–260 T across the molding floor, including automated vertical cells for insert molding, LSR and precision thermoplastic parts.
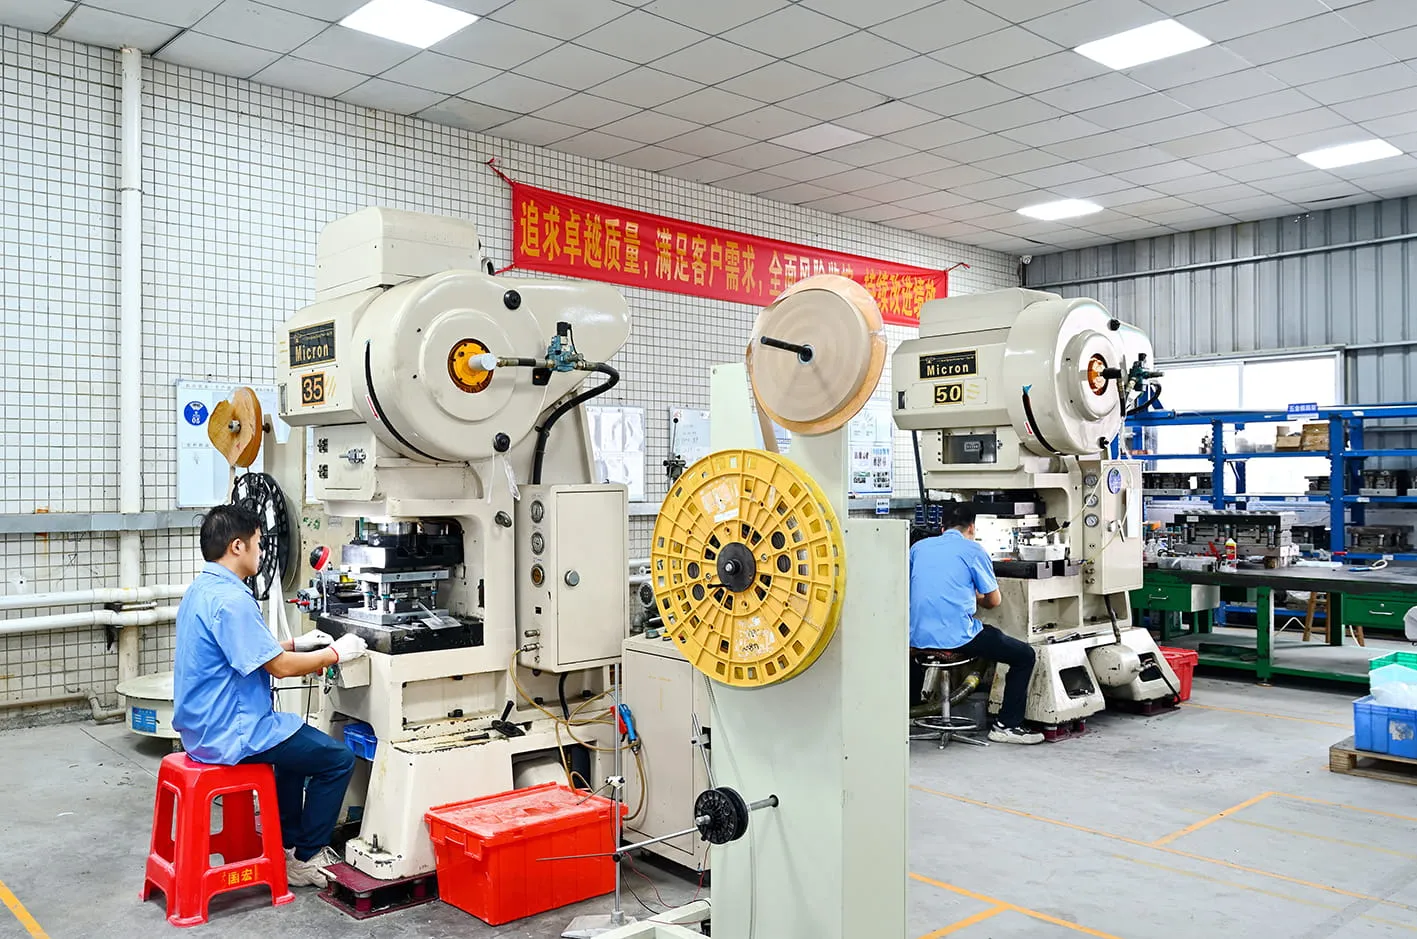
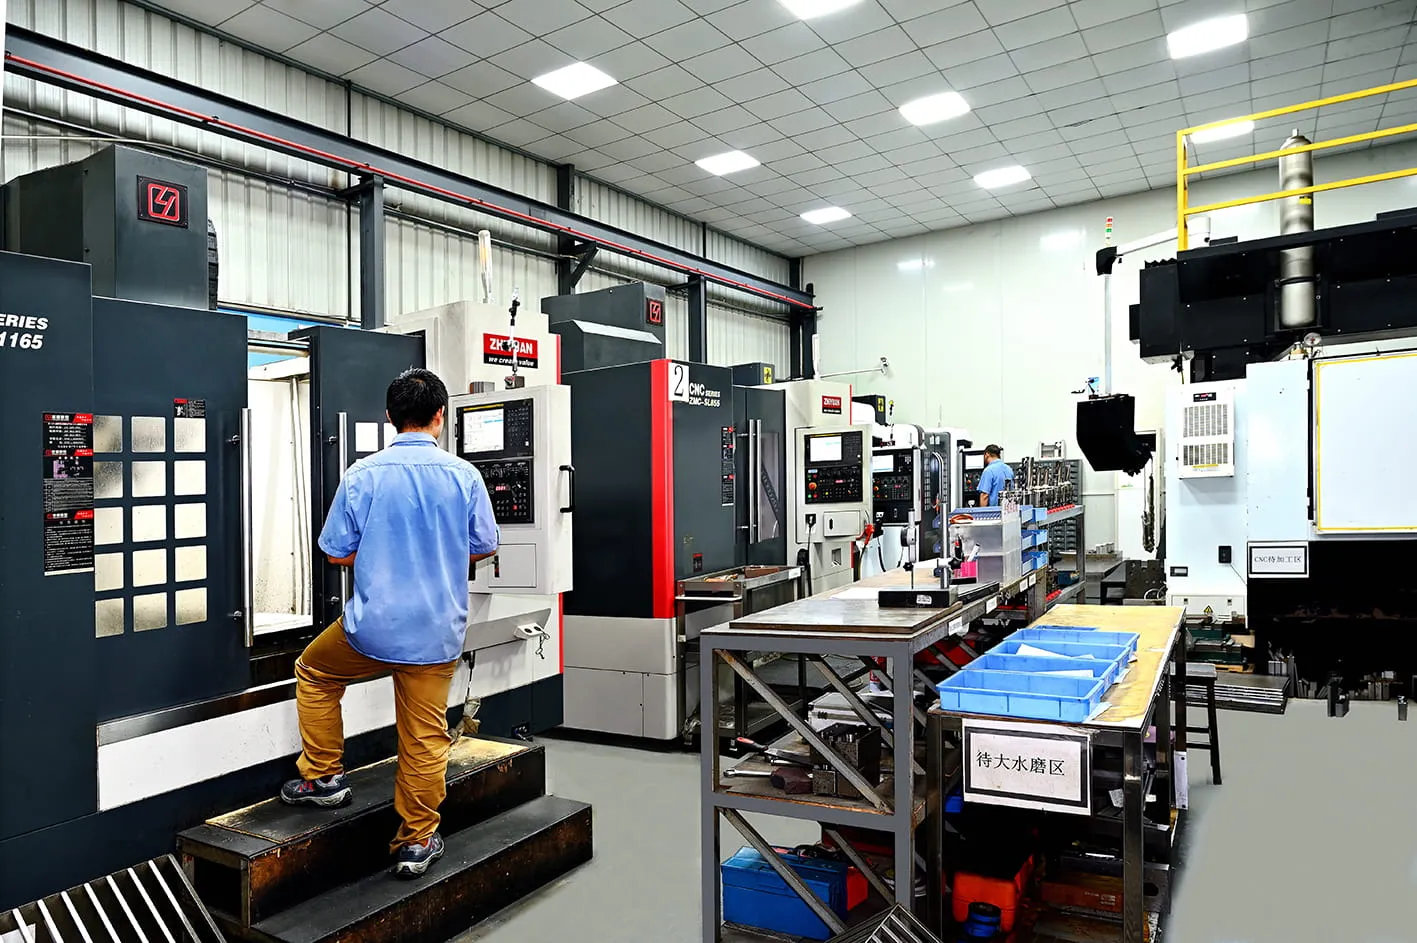
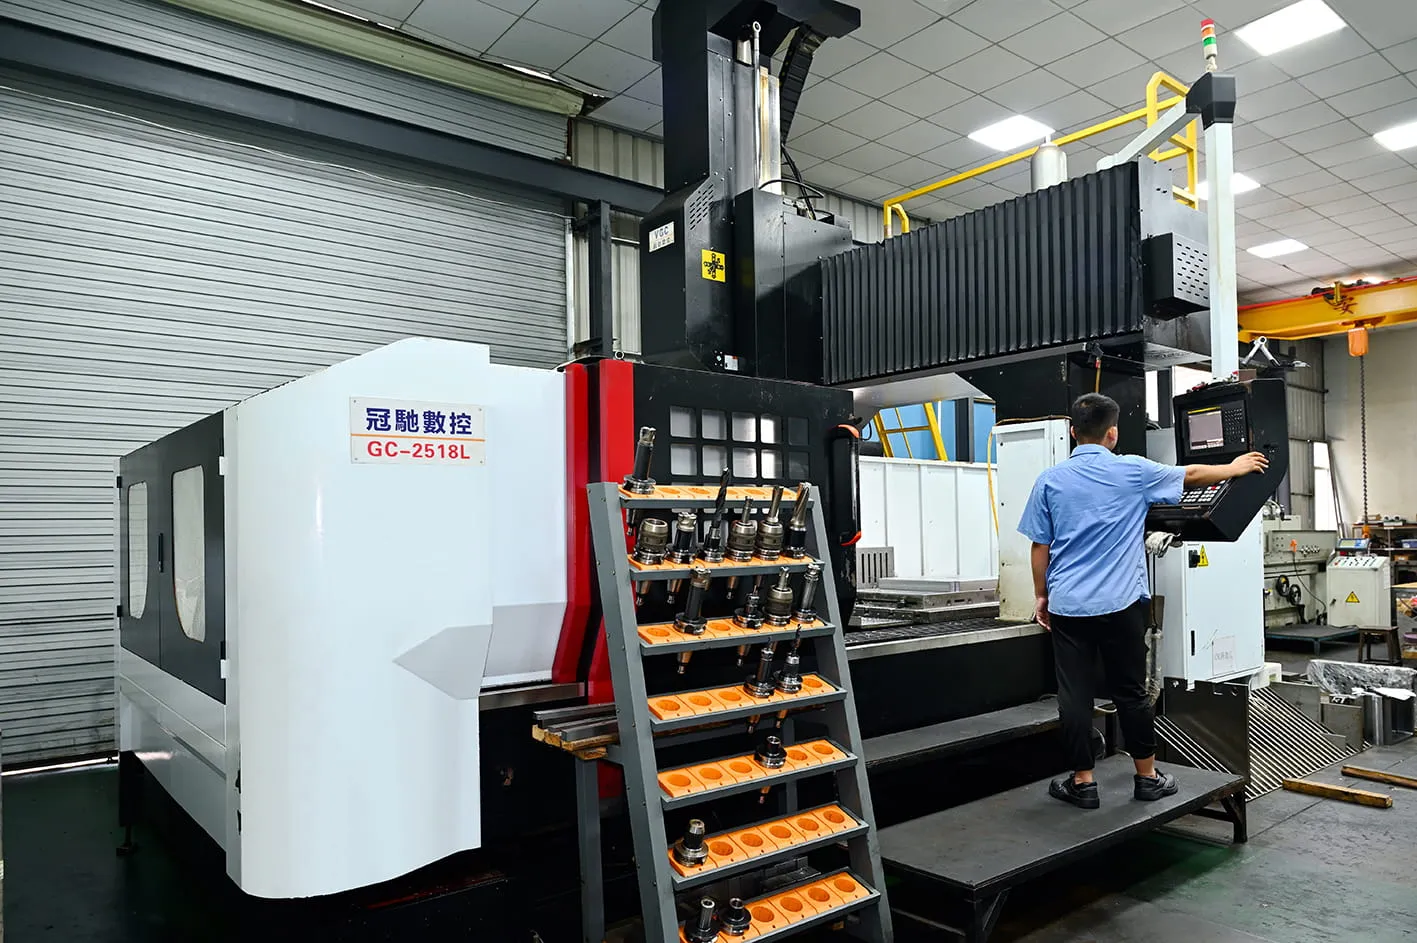
Stamping & CNC Workshop
21 high-speed stamping presses (25–110 T) for metal inserts and brackets, alongside CNC machining holding ±0.005 mm.
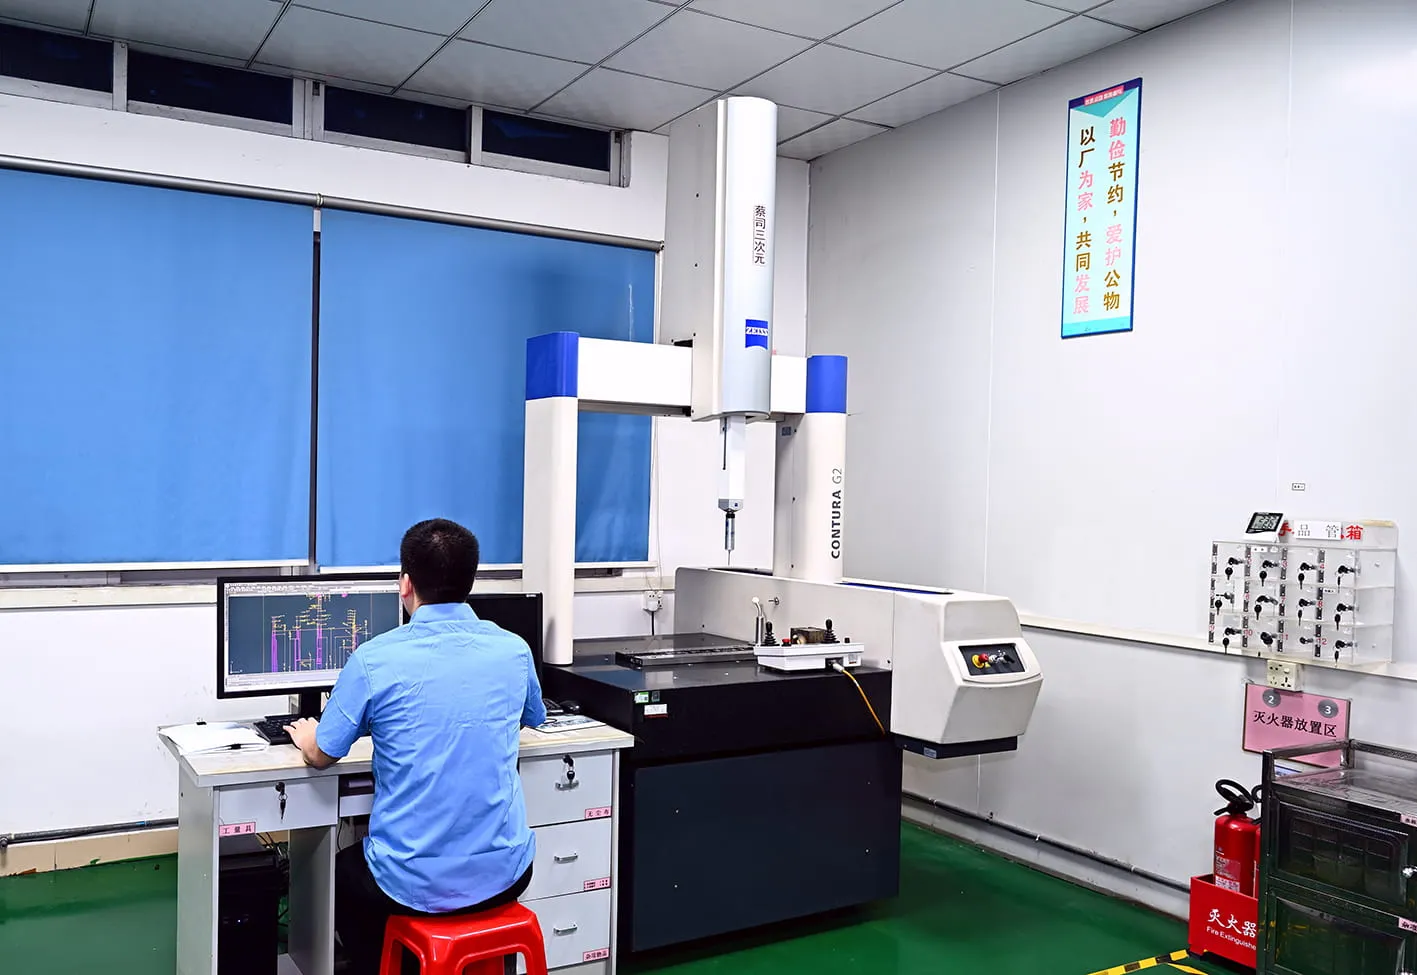
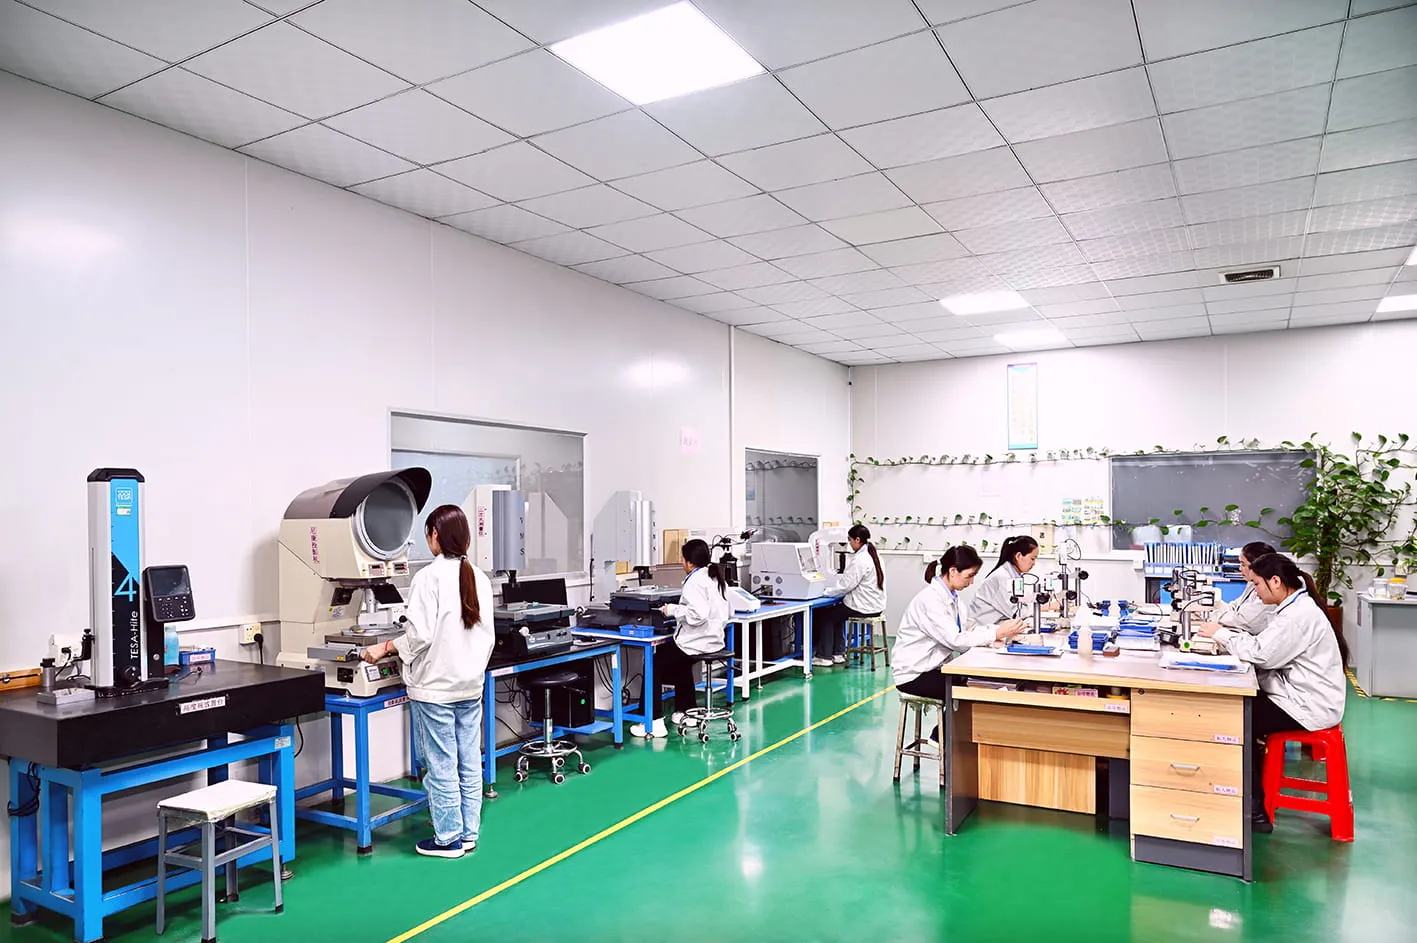
Quality Control Lab
CMM, vision measurement and in-process sampling — every program ships with dimensional inspection data.
Every Program Under One Quality System
The biggest cost in a molded part is rarely the plastic — it is the hand-offs. When tooling, molding, stamping and inspection are split across suppliers, every transfer adds freight, lead time, communication overhead and a new place for tolerances to drift. Our factory is organized the opposite way: molding, stamping, CNC and inspection workshops run under one quality system and one ERP, with tooling managed by the same accountable team.
That structure is why we can move from DFM review to first articles without shipping a single file folder. It is also why a design change during tooling costs hours, not weeks — the toolmaker, process engineer and QC inspector report to one accountable team. You can see the mold making process and how parts are injection molded end to end.
Equipment & Capacity
- Injection molding: injection presses spanning 30–260 T, with the vertical molding line running insert molding to ±0.02 mm insert positioning.
- Wire EDM & tooling: wire-cut and die-sinking EDM capability, backed by CNC milling for cavities and inserts.
- Stamping: 21 high-speed presses (25–110 T) producing metal inserts, brackets and terminals on-site.
- CNC machining: precision milling and turning holding ±0.005 mm, used for prototypes, tooling components and machined parts.
- Workforce: 280 employees across tooling, molding, stamping, finishing and quality.
Capacity planning is straightforward for buyers: low-volume runs quote at 7–12 days and mass production at 25–30 days, with global shipping from Dongguan. Comparable on-site factories quote 50–10,000 low-volume parts in about 15 days — a good sanity check for the lead-time range an on-site factory should be quoting.
Full Equipment Inventory
| Process | Machines on floor | Capacity notes |
|---|---|---|
| Injection molding | 30–260 T injection presses · automated vertical insert-molding cells | Horizontal line runs production molding; vertical line runs insert molding and LSR |
| Tooling & EDM | Wire-cut EDM · die-sinking EDM · CNC milling | Electrodes, punch and die steel, complex cavity work — tooling programs run through an audited tooling partner network |
| CNC milling & turning | High-speed CNC machining centers · gantry mills · precision turning lathes | Mold plates, inserts and ±0.005 mm machined parts; also CNC prototype runs |
| Grinding & finishing steel | Surface grinders (Mitsui, Wasino GLS-5T optical profile) · centerless grinder | Ground details for punch and die steel, hardened insert faces |
| Stamping | 21 high-speed presses, 25–110 T (incl. gantry feed lines) | Metal inserts, terminals and brackets feeding insert molding the same day |
| Secondary ops | Ultrasonic welding · terminal grinding · pad-printing/finishing lines | Welded assemblies and marked parts without shipping out |
| Metrology | Zeiss CMM · 2D optical projectors · Trimos height gauges · hardness, coating-thickness, force and leak-test benches | Full dimensional and functional reports — see the quality control page |
Why Facilities Matter to Your Program
Facilities are not decoration — they are a risk map. One accountable tooling program means your mold is not hostage to a supplier backlog. Stamping on our site means metal inserts arrive when molding needs them, not when a supplier ships them. An on-site QC lab means first articles are measured before the press runs a thousand parts, not after. Learn how those checks are structured on our quality control page, or read about the company behind the factory on the about page.
Frequently Asked Questions
Can you make both the mold and the parts?
Yes — we deliver mold design, mold build and molding as one accountable program under one quality system, from DFM to the first production shot.
What machine sizes do you run?
Horizontal presses from 40 to 100 tonnes and vertical presses from 45 to 120 tonnes — a 30–260 tonne range covering small precision parts through medium housings and insert-molded components.
Do you do metal stamping on-site?
Yes, 21 high-speed presses produce inserts, brackets and terminals on-site, so insert molding does not depend on an outside stamping supplier.
How fast are low-volume lead times?
Low-volume runs typically ship in 7–12 days and mass production in 25–30 days, depending on part geometry, material and finish.